Best Stack Light With Buzzer for Industrial Alerts and Visual Signals
Stack lights with buzzers provide clear, multi-color signaling for machines, workstations, and production lines. This article highlights five top options with audible alerts, sturdy construction, and flexible mounting to help operators quickly identify status, warnings, and process conditions. Whether you need a compact two-layer unit or a full four-layer tower, these selections cover a range of voltages, mounting styles, and durability features for industrial environments.
| Product | Key Features | Notes |
|---|---|---|
| ANDONT 3 Stack LED Andon Tower Lights with Buzzer | 3-color stack, buzzer, 16 ft cord, IP53 | Plug-and-play setup |
| ATO Stack Light with Buzzer, 5 Layers | 5 colors, detachable modules | Suitable for operator stations |
| LUBAN Industrial Signal Tower, 2-Layer | 2-layer, built-in buzzer, bright LEDs | Durable mount and 90 dB buzzer |
| LUBAN Led Signal Tower Stack Lights, 1-Layer (With Buzzer) | 1-layer, 90 dB buzzer | Compact option with audible alert |
| ANDONT 4 Stack LED Andon Tower Light with Buzzer | 4-color, 85 dB buzzer, plug & play | Industrial-grade with 6 ft adapter |
ANDONT 3 Stack LED Andon Tower Lights with Buzzer

This triple-stack tower uses red, yellow, and green LEDs with an integrated buzzer. The device includes a 16 ft extension cord and a 6 ft industrial adapter, making it suitable for factory floors and workshop areas. Its IP53 rating provides resistance to dust and light water exposure. The unit supports a default switch configuration for buzzer, red flash, yellow on, and green on, delivering both visual and audible alerts for operators.
ATO Stack Light with Buzzer, 5 Layers
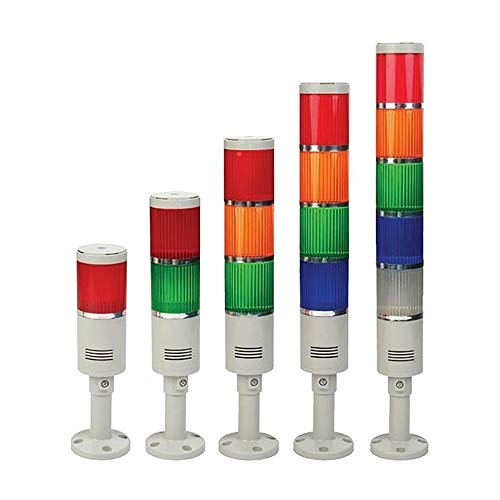
ATO’s stack light features five color layers and a detachable module design for easy service and customization. The polycarbonate shell offers clear color transmission and durability for demanding environments. It is well-suited for operator stations, call lights, and machine monitoring, delivering reliable status indications in warehouses or production lines where quick visibility and loud alerts are critical.
LUBAN Industrial Signal Tower, 2-Layer with Buzzer

This two-layer stack light combines bright LEDs with a built-in 90 dB buzzer for immediate audible notification. A robust build uses PC lamp shades and ABS bodies with an aluminum support rod, offering reliable mounting and visibility for safety signaling on shop floors or control panels. It’s designed for long-term operation and straightforward installation in industrial settings.
LUBAN Led Signal Tower Stack Lights, 1-Layer (With Buzzer)

This compact, single-layer stack light includes a 90 dB buzzer for audible alerts and is designed for environments where space is at a premium. It provides clear visual indication with steady or flashing light modes and is suitable for smaller control panels, operator desks, or compact machinery signaling needs.
ANDONT 4 Stack LED Andon Tower Light with Buzzer

This four-layer signal tower provides Red, Yellow, Green, and Blue LEDs with an integrated buzzer (85 dB). It features plug-and-play installation with a 6 ft industrial power adapter and a 4-hole control box. Its robust design supports 85–264V AC for broad industrial compatibility, delivering rapid, multi-color status signals across large operations or dense production lines.
Buying Guide: Key Purchase Considerations
When selecting a stack light with a buzzer, consider the following factors to match your application and environment:
- Number of layers/colors: Choose 2, 3, or 4 layers based on the complexity of statuses you need to convey.
- Buzzer level and sound type: Look for decibel ratings (e.g., 85–90 dB) and whether the buzzer emits continuous, intermittent, or pulsing alerts to suit the workspace.
- Voltage and power requirements: Verify input voltage compatibility (AC 110–264V or DC options) and whether a plug-and-play adapter is included.
- Durability and enclosure: Consider IP ratings (IP53 or higher) for dust and splash resistance, as well as housing materials for industrial environments.
- Mounting and space: Assess the footprint, height, and whether a rotatable base or adjustable pole is needed for optimal visibility.
- Connectivity and compatibility: Ensure the control box and selector switches align with your existing control systems and safety protocols.
- Maintenance and serviceability: Detachable modules or quick-disconnect wiring can reduce downtime during maintenance or color changes.
- Color visibility and light intensity: High-visibility LEDs and 360-degree visibility improve quick recognition on busy floors.
- Compliance and safety: Look for products meeting applicable electrical and safety standards for your country and industry.
- Longevity and warranty: Choose units with long LED lifespans and reliable manufacturer support to minimize replacement costs.